EWAC ALLOYS PRODUCTS
EWAC Alloys manufactures welding consumables, repair alloys and wear-resistant solutions. CPEM 021 is a high-strength electrode for joining manganese steel, low alloy steel and medium carbon steel, with applications in construction and mining equipment repair.

CPEM 021 Electrode
CPEM 021 is an EWAC high-strength electrode for joining manganese steel, low alloy steel and medium carbon steel. It combines low heat input, high ductility and excellent crack resistance for demanding repair and joining applications.
Product Description
CPEM 021 ac/dc+ is an electrode for high-strength joining of manganese steel, low alloy steel and medium carbon steel. It is designed for demanding joining and repair work where low heat input, high ductility and crack resistance are important.
The electrode is recommended for similar and dissimilar combinations of low-medium carbon steels, low alloy steels and manganese steels encountered in construction and mining industries.
During welding, the job temperature should be controlled to prevent localized heat build-up. For manganese steel, EWAC recommends not allowing the job temperature to exceed 150°C.
Product type – high-strength steel welding electrode. Process – AC/DC+. Product designation – CPEM 021 ac/dc+.
Applications
- Buckets of earthmoving equipment
- Booms and sticks
- C frames and undercarriage components
- Construction equipment repair
- Mining equipment repair
- Joining similar and dissimilar low-medium carbon, low alloy and manganese steels
Key Features & Benefits
- Low heat input
- Compatible with a wide range of steels
- High ductility
- Excellent crack resistance
- Suitable for similar and dissimilar steel combinations
- Suitable for manganese steel joining and repair
- Recommended for construction and mining equipment applications
- Available in 3.15, 4.00 and 5.00 mm sizes
Technical Data
| Product | CPEM 021 ac/dc+ |
| Product Type | High-strength steel welding electrode |
| Process | AC/DC+ |
| Base Materials | Manganese steel, low alloy steel and medium carbon steel |
| Tensile Strength | 59 kg/mm² (84,000 psi) |
| Electrode Size | 3.15 mm |
| Recommended Amperage | 55–100 A |
| Electrode Size | 4.00 mm |
| Recommended Amperage | 85–140 A |
| Electrode Size | 5.00 mm |
| Recommended Amperage | 135–185 A |
| Recommended Job Temperature for Mn Steel | Do not allow job temperature to exceed 150°C |
Related EWAC Products
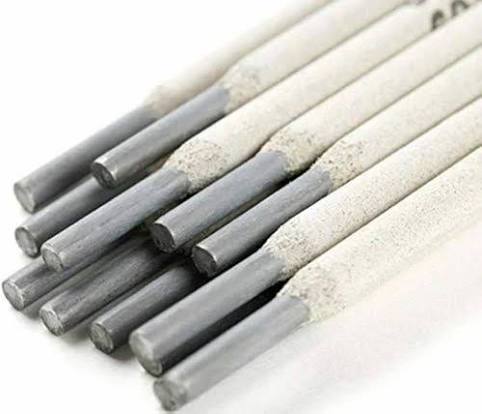
UNITRO U Electrode
Specialized ac/dc+, high-alloy welding electrode
- For joining a wide range of stainless and mild steels
- Excellent oxidation and heat resistance
- Suitable for valves, tanks and heat exchangers
- Typical tensile strength: 69 kg/mm² (97,500 psi)
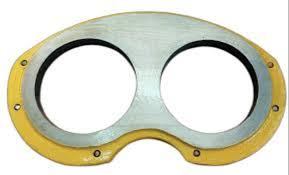
EDP 550 Wear Plate
Weld-cladded, iron-chromium-carbon alloy wear plate
- High wear resistance for severe abrasion conditions
- Iron-chromium-carbon alloy weld-cladded plate
- Designed for protection of high-wear surfaces
- Suitable for demanding industrial wear applications
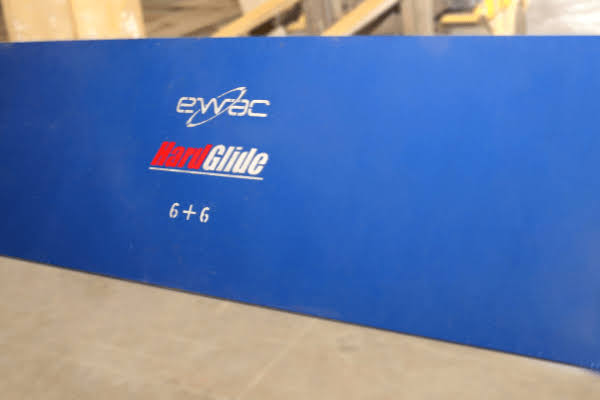
HardGlide Wear Plate
Revolutionary, ultra-abrasion-resistant overlay wear plate
- Ultra-abrasion-resistant hardfacing overlay
- Designed for severe wear environments
- Provides long-lasting surface protection
- Suitable for industrial wear and maintenance applications
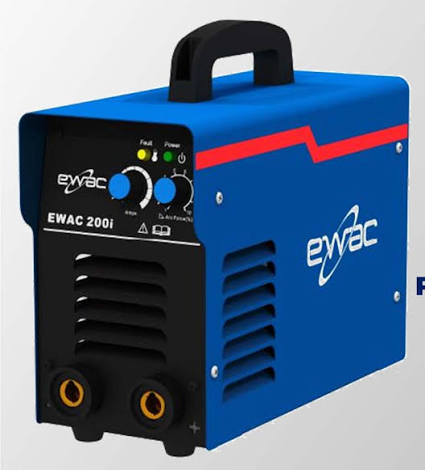
Ewac 200i Welding Machine
Advanced, IGBT-based, single-phase portable welding inverter
- IGBT-based welding inverter technology
- Single-phase and portable design
- Suitable for welding and maintenance applications
- Compact solution for convenient site welding