EWAC ALLOYS PRODUCTS
EWAC Alloys manufactures welding consumables, repair alloys and wear-resistant solutions. CPCI 026 is an excellent electrode for repair of cast iron casting defects and machine build-up, delivering dense deposits with good bonding and optimum machinability.
CP CI 026 Electrode
CPCI 026 is an EWAC cast iron welding electrode designed for foundry defect repair, machine build-up, rectification of machining errors and rebuilding worn cast iron parts.
Product Description
CPCI 026 ac/dc- is an excellent cast iron welding electrode for repair of casting defects and machine build-up. It produces dense deposits with good bonding and offers optimum machinability.
It is recommended for weld repair of foundry defects such as blow holes, shrinkage, cavities and missing sections where a sound machinable deposit is essential. It is also suitable for rectification of machining errors and for building up worn-out areas of cast iron parts.
Preheating is normally not required, but may be employed up to 150°C for better machinability. Welding should be performed using minimum current and a short arc gap, with stringer beads and peening after each bead.
Product type – cast iron welding electrode. Process – AC/DC-. Product designation – CPCI 026 ac/dc-.
Applications
- Foundry defect repair
- Machine build-up
- Repair of blow holes
- Repair of shrinkage and cavities
- Rectification of machining errors
- Building up worn-out cast iron parts
- Slurry pump repair
- Cast iron maintenance and repair applications
Key Features & Benefits
- Excellent operating characteristics
- Dense deposits with good bonding
- Optimum machinability
- Stronger than conventional nickel-based cast iron welding alloys
- Suitable for foundry defect repair
- Suitable for machine build-up and worn-part restoration
- Suitable for rectification of machining errors
- Available in 2.5, 3.15 and 4.00 mm sizes
Technical Data
| Product | CPCI 026 ac/dc- |
| Product Type | Cast iron welding electrode |
| Process | AC/DC- |
| Base Material | Cast iron |
| Tensile Strength | 42 kg/mm² (60,000 psi) |
| Electrode Size | 2.5 mm |
| Recommended Amperage | 50–60 A |
| Electrode Size | 3.15 mm |
| Recommended Amperage | 60–85 A |
| Electrode Size | 4.00 mm |
| Recommended Amperage | 85–110 A |
| Preheating | Normally not required; may be employed up to 150°C for better machinability |
| Typical Applications | Foundry defects, machine build-up, machining error rectification and worn cast iron parts |
Related EWAC Products
CPEM 021 Electrode
Specialized AC/DC+ welding electrode
- High-strength welding electrode
- For demanding repair applications
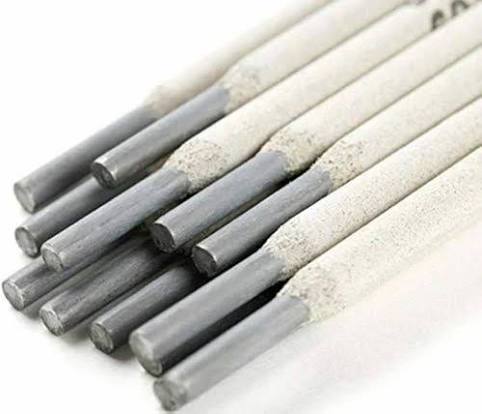
UNITRO U Electrode
Specialized ac/dc+, high-alloy welding electrode
- High-alloy welding electrode
- For steel joining applications
Terra CI 94 Electrode
Specialized ac/dc, machinable cast iron welding electrode
- Machinable cast iron electrode
- For cast iron joining and repair
HardGlide Wear Plate
Revolutionary, ultra-abrasion-resistant overlay wear plate
- High-performance wear protection
- For demanding abrasion applications